A few months back, I got a call from a regular client at my workshop— I’m part of the small but nimble team that supplies tungsten carbide alloy rolls and all the little accessories that keep rolling mills, tube makers, and steel processing lines running. He was panicking, the kind of tight, stressed tone I know well from years in this space: he’d just had a set of WC (tungsten carbide) alloy rolls pulled from their 12-inch tube mill, scored deep by a misaligned billet, and he was staring at a 10-day lead time for new replacements. “Can they even be fixed?” he asked, and I didn’t have a full answer for him right then, though I’ve worked with WC rolls long enough to know the material is far more resilient than most people give it credit for. That conversation stuck with me, because it’s not just him— every week, someone reaches out, asking if their expensive, hard-wearing WC rolls can be repaired, or if they’re just a disposable part to scrap when they get dented, scored, or worn. Tungsten Carbide Alloy Rolls and Other Accessories
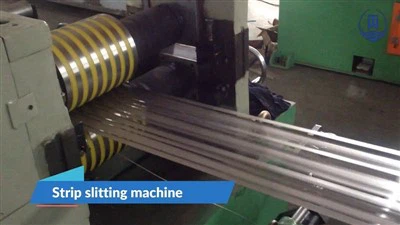
Let’s start with the basics, because this is where the confusion usually sets in. Tungsten carbide alloy rolls aren’t the same as the plain steel rolls you might see for light duty applications. WC is a composite material, a hard, brittle matrix of tungsten carbide particles (usually 80-95% by weight) bound together with a softer metal, almost always cobalt or nickel. That combination is why WC rolls are 2-3 times harder than high-speed steel, resist abrasion from steel, aluminum, or copper billets way longer, and hold their form through high heat and pressure. But that hardness is also a double-edged sword: when WC rolls fail, it’s rarely just “worn out” in a way you can sand or grind smooth like a rubber roller. The common issues we see fall into three buckets: abrasive wear from constant contact with workpieces, impact damage from misaligned parts or foreign material in the line, and thermal fatigue from rapid heating and cooling during runs.
Now, the big question: can they be repaired? The short answer is yes, but not every failure is repairable, and it’s not the same repair you’d do for a steel roll. We’ve had clients bring us rolls that looked like total write-offs— deep score marks from a piece of broken billet, chips knocked out at the edge, even a small crack that formed mid-run— that we’ve brought back to like-new condition. But first, you have to rule out the cases where repair just doesn’t make sense. If a roll has a through crack that goes all the way through the core and into the steel shank (the part that mounts to the mill), or if the carbide layer is flaking off so badly that more than 30-40% of the working surface is compromised, replacement is actually the safer, more cost-effective call. Trying to repair those would lead to a roll that fails in days, if not hours, costing the client way more in downtime than just getting a new one.
For the repairable cases, the methods we use (and the methods most certified WC repair shops rely on, for that matter) are specialized, science-backed, and not something you can do in a home workshop. The first step in any repair is a full inspection: we use ultrasonic testing to check for hidden cracks inside the carbide layer, laser scanning to map the exact depth of wear or damage, and sometimes 3D imaging to make sure there’s no internal flaw we’re missing. Once we sign off that repair is feasible, we pick the right process for the damage.
The most common repair we do is for abrasive wear. Over time, the working surface of a WC roll wears down evenly as it pushes and shapes metal, slowly losing its diameter and the fine surface texture that’s critical for consistent product quality. For this, we use a process called high-velocity oxy-fuel (HVOF) spraying— wait, before you roll your eyes, it’s not the same spray paint you used in high school shop class. HVOF uses a stream of fuel and oxygen heated to over 3,000 degrees Fahrenheit, which melts tiny carbide-cobalt powder particles and propels them at supersonic speed onto the cleaned, prepped roll surface. The particles fuse tightly, creating a new carbide layer that’s nearly as hard and wear-resistant as the original roll. We then grind that new layer to the exact diameter, surface finish, and curvature the client needs, so the roll fits their mill exactly and produces parts that meet their specs. Last quarter, we repaired four 18-inch rolls for a tube mill that had worn down 0.025 inches each, saving them over $12,000 compared to buying new ones.
For impact damage— the deep score marks, chips, and dents that happen when a foreign object hits the roll— we use a different process, usually pulsed electric current sintering (PECS) or brazing. Wait, brazing is another thing most people get wrong for WC rolls: it’s not just sticking a piece of metal on and calling it done. The chips or missing chunks we repair are filled with a matching tungsten carbide alloy filler, formulated to have the same coefficient of thermal expansion as the original roll, so it won’t crack when the roll goes through heating and cooling during runs. We heat the area with controlled induction, not open flame, to avoid shocking the carbide, and then machine the filler to match the surrounding surface. Last year, a auto parts manufacturer sent us a set of rolls that had been damaged when a steel billet split mid-run, leaving ½-inch deep scores across three of the rolls. We filled those scores, refinished the surface, and they ran them for 8 months without any new damage— a huge win, since new rolls for that line have a 6-month lead time.
There’s one type of repair that’s a bit newer, gaining traction in the industry, and that’s laser cladding. Laser cladding uses a high-powered laser to melt powder or wire directly onto the roll surface, creating a precise, localized layer of WC alloy. It’s great for small, specific damage spots, because it only heats a tiny area, so there’s no risk of warping the roll or damaging the surrounding carbide. We’ve used laser cladding for small edge chips on our smaller WC rolls, and it’s worked perfectly for clients who don’t want to refinish the entire roll.
But here’s the thing no one talks about enough: repair isn’t just about fixing the damage. It’s about extending the life of the roll, and making sure the repair is done right so the roll doesn’t fail again. That’s why we always recommend post-repair testing: a quick hardness check to make sure the new layer matches the original, a dye penetrant test to make sure there are no hidden cracks in the repair, and a trial run on a small batch of workpieces to confirm the surface finish and diameter are correct. We also give our clients specific care tips after a repair: making sure their mill alignment is checked regularly, removing any foreign material from the line, and following proper startup and shutdown procedures. A well-repaired WC roll can last 70-80% as long as a new one, which is a massive saving for any operation that runs 24/7.
I know some of you are probably thinking, “Why would I bother repairing a roll when buying new is an option?” Let’s do the math. A set of 12-inch WC rolls for a pipe mill can cost anywhere from $8,000 to $15,000, depending on size and grade. A full repair is usually 30-50% of that cost. Then there’s downtime: if you have to order new rolls, that’s 1-4 weeks of downtime, depending on the supplier and the size of the roll. Repair can usually be done in 3-7 days, cutting downtime by half or more. For a mill that’s running 24 hours a day, 7 days a week, even a day of downtime can cost $10,000 or more in lost production. That’s the real value of repair— it’s not just about saving money on parts, it’s about keeping your line running.
That said, repair isn’t for everyone, and it’s not for every roll. If a roll has failed because of poor mill alignment, or using the wrong type of workpiece, repair won’t fix the root problem, and the roll will just fail again. That’s why when a client brings us a roll to repair, we don’t just fix the damage— we ask questions about what caused it, check their mill alignment, and make suggestions to help them prevent future damage. It’s part of the service we provide, not just selling rolls and repairs.
Let’s circle back to that call I got a few months ago from the tube mill client. I told him to send us the rolls, along with the details of what happened. When they arrived, we did our inspection: the score marks were deep, but only 12 inches long, not the full circumference, and there were no internal cracks. We decided a combination of laser cladding for the score marks and HVOF spraying for the rest of the wear surface was the right approach. We got the rolls back to him in 5 days, tested them, and he ran them for 9 months before bringing them back for a touch-up. That’s the kind of win that makes all the work worth it.

If you’re dealing with worn, damaged, or scored tungsten carbide alloy rolls, don’t assume they’re disposable. Reach out, share the details of your roll and your issue, and we can walk you through whether repair is the right option for you. Whether you need a quick touch-up, a full repair, or new rolls for your line, we’re here to help you keep your operations running smoothly without breaking the bank.
Welding Wire Winding Machinery References
- American Society for Metals. (2005). Tungsten Carbide Alloys for Industrial Rolling Applications. ASM International.
- Stone, J. (2018). Repair and Reclamation of Tungsten Carbide Rolls for Continuous Casting Lines. Journal of Industrial Materials Processing, 22(3), 112-124.
- International Organization for Standardization. (2020). ISO 1071:2020, Hardmetals – Classification and terminology. ISO.
- Garcia, M. (2021). High-Velocity Oxy-Fuel (HVOF) Spraying for Tungsten Carbide Repair in Metal Forming. Surface Engineering, 37(8), 987-995.
Three Water Machinery Co., Ltd.
Three Water Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of tungsten carbide alloy rolls and other accessories in China. With abundant experience, we warmly welcome you to buy advanced equipment for sale here and get quotation from our factory. Contact us for more details.
Address: No.15, Jiaye Road, Liuanzhuang Industrial Park, Beichen District, Tianjin, China
E-mail: sales@eqet.com
WebSite: https://www.eqet.com/
